
BuildMEP fixed gas-detection field guide
Use this guide to diagnose unreliable combustible-gas detectors and to verify the complete path from gas reaching the sensor to alarm, operator action and any required shutdown.
Decision brief: prove the detection function, not only the transmitter
A normal display or a recently signed calibration sheet does not prove that a combustible-gas detection system will respond to a real release. Reliability depends on four linked conditions:
- the selected sensing technology responds to the actual target gas and operating atmosphere;
- the release plume can reach the sensor within the required time;
- the sensor, transmitter, cabling, controller, alarm and interlock respond end to end; and
- the maintenance method detects poisoning, obstruction, drift and incorrect restoration.
When a detector gives weak response, repeated calibration demand or unexplained zero readings, stop treating calibration as the default repair. Identify which part of that chain has failed.
Start with the sensing technology and target gas
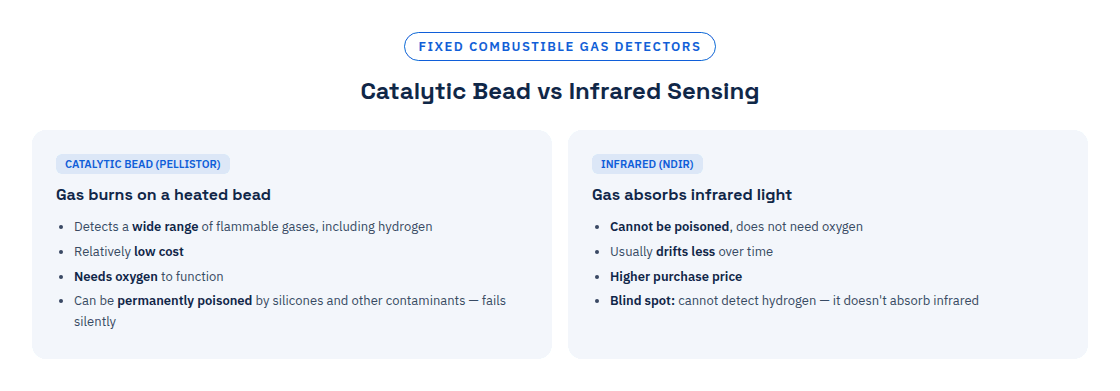
Most fixed lower explosive limit (LEL) point detectors use catalytic-bead or infrared sensing. Neither is universally better. Selection must follow the target-gas list, oxygen conditions, likely contaminants, required response, environmental limits and the manufacturer’s performance data for the exact sensor.
| Check | Catalytic bead | Infrared | Design implication |
|---|---|---|---|
| Measurement principle | Oxidation on a heated catalyst changes element resistance. | Target molecules absorb selected infrared wavelengths. | Confirm that the certified gas list and response data include the project gases. |
| Oxygen dependency | Requires sufficient oxygen for the catalytic reaction. | Does not rely on oxygen for the optical measurement. | Do not assume a catalytic detector remains valid in inerted or oxygen-deficient service. |
| Poisoning and inhibition | May be permanently poisoned or temporarily inhibited by contaminants; susceptibility is product-specific. | No catalyst to poison, but optics can be obscured and the device can still fault or drift. | Review chemicals, sealants, lubricants, dust, condensation and cleaning products around the sensor. |
| Hydrogen | Products are available that respond to hydrogen when used within their approved conditions. | Conventional hydrocarbon IR sensors do not detect hydrogen. | If hydrogen is credible, verify an explicitly approved hydrogen technology rather than assuming “LEL” means all fuels. |
| Typical diagnostic clue | Slow or low gas response after contaminant exposure; increasing span demand. | Beam or optical fault, contamination indication, or response mismatch for an unsupported gas. | Use the product manual’s fault codes and response limits before replacing or recalibrating. |
Why a healthy display can hide an unavailable detector
A fault monitor can identify some electrical and optical failures, but it cannot prove that the target gas reaches the detector or that the sensor still responds correctly. HSE guidance explicitly includes incorrect positioning, maintenance quality, calibration, performance testing, proof testing and alarm response among the reliability questions for leak and gas detection.
Field note: treat contaminant exposure as an event
Silicones, silicates, lead compounds, sulfur compounds and halogenated materials can desensitize certain catalytic sensors. The exact list and effect vary by product. When a new sealant, lubricant, coating or cleaning chemical is introduced near a catalytic detector, record the exposure and perform the manufacturer’s prescribed response check. Do not compensate for a persistently weak sensor by repeatedly increasing span gain.
Bump test, calibration and proof test are different jobs
| Activity | What it checks | What it does not prove by itself | Required record |
|---|---|---|---|
| Visual inspection | Condition, orientation, obstruction, water, dust, damage, access and identification. | Gas response or measurement accuracy. | Observed condition and correction. |
| Bump or response test | Known gas reaches the sensor and produces a response; the defined test may also verify local alarms. | Full measurement accuracy unless the manufacturer defines and passes an acceptance tolerance. | Gas, concentration, cylinder expiry, response, alarm operation and pass criterion. |
| Calibration | Zero and span are adjusted or verified against specified gas under the product procedure. | Detector placement, real plume travel, remote alarm delivery or final shutdown action. | As-found and as-left values, gas, flow, adapter, result and technician. |
| End-to-end proof test | The sensor, transmitter, wiring, controller, alarm, interlock, final action and feedback operate as intended. | Coverage for every credible release unless the test and study address those scenarios. | Initiating stimulus, response times, outputs, bypasses and restoration to service. |
Do not copy a test interval from another detector
Test and calibration frequency must follow the exact manufacturer’s instructions, the site’s risk assessment, contaminant exposure, environmental severity, performance history and governing requirements. Guidance for portable detectors often recommends a bump test before each day’s use; that is not automatically the maintenance interval for every continuously operating fixed detector. After a failed test, significant contaminant exposure, over-range event, repair or sensor replacement, follow the product-specific recovery and verification procedure before returning the point to service.
Placement: gas density is a starting input, not the design
The common rule—high for lighter-than-air gases and low for heavier-than-air vapours—can help frame a first review, but it cannot determine coverage alone. A pressurized or refrigerated release may initially behave differently from the pure gas at ambient conditions. Ventilation, thermal currents, wind, congestion, doors, drains, pits and equipment geometry can dominate plume travel.
Start at credible release points such as seals, valve stems, flanges, hose connections and drains. Then trace where the gas could accumulate, where people or critical equipment may be exposed, and how ventilation changes in normal, standby and failure modes. The detector must remain accessible for the specified test method without creating an unsafe maintenance task.
Placement review questions
- Which gas or mixture controls the detector technology and calibration basis?
- What release locations, rates, pressures, temperatures and operating states are credible?
- Where do supply air, extraction, open doors and natural convection carry the plume?
- Could water, dust, paint, insulation, stored materials or insect ingress block the inlet?
- Can the specified gas, adapter and flow reach the sensing element during routine testing?
- Does the coverage objective protect a leak source, an occupied zone, an air intake, an escape route or a shutdown function?
A disciplined troubleshooting sequence
- Make the area safe. Apply the site’s gas-testing, permit, isolation and hazardous-area procedures. If a detector is unavailable, define temporary protection or remove the hazard before maintenance.
- Check the history. Review target gas, sensor model, installation date, recent alarms, contaminant exposure, over-range events, last as-found result and repeated span adjustments.
- Inspect the gas path. Confirm the weather guard, sinter, calibration port, remote tubing, filters and inlet are clean, dry, correctly assembled and suitable for the target gas.
- Verify the test equipment. Confirm gas identity and concentration, cylinder expiry, regulator type, flow, tubing material, adapter fit and safe exhaust route against the manual.
- Apply known gas and record response. Capture response time, indicated value, stability and local alarm—not only pass/fail. A slow or low response is diagnostic evidence.
- Separate sensor from loop faults. Follow the manufacturer’s permitted substitution or simulator method in a safe condition. Do not hot-swap uncertified parts or open explosion-protected equipment while energized.
- Test the remote path. Confirm controller input, alarm priorities, beacons, BMS/DCS indication, interlocks, shutdowns and feedback. Record every inhibited output and restore it deliberately.
- Decide repair, replacement or redesign. Replace a sensor that cannot meet response limits; repair wiring or electronics when the sensor is sound; redesign placement or technology when the release cannot reliably reach or be measured by the point.
Failure-mode register
| Cause or mistake | Consequence | Field symptom | Correction |
|---|---|---|---|
| Catalytic contaminant exposure | Reduced or lost gas response. | Slow bump response, low reading or increasing span demand. | Confirm exposure, test to the manual, replace if limits are not met and control the contaminant source. |
| Wrong calibration gas or unsupported cross-calibration | Biased indicated %LEL for the target gas. | Good response to test gas but inconsistent process response. | Use the specified gas or the manufacturer’s documented response factor and conditions. |
| Expired gas, wrong flow or leaking adapter | False low exposure during service work and incorrect adjustment. | Unstable reading or excessive gain required. | Replace gas or test hardware; repeat an as-found test before adjusting. |
| Obstructed guard, sinter or sample line | Delayed or absent response. | Slow response with otherwise stable electronics. | Clean or replace only by the approved procedure; verify the entire gas path afterward. |
| Placement based only on vapour density | Plume bypasses the sensor. | Nearby portable instrument alarms while the fixed point remains low. | Reassess release sources, airflow and accumulation; perform a coverage study where warranted. |
| Calibration before stabilization | Zero or span shifts after service. | Point passes, then drifts after warm-up. | Observe the exact power-up and stabilization time in the product manual. |
| Unverified wiring or shield termination | Noise, offset, intermittent faults or loss of signal. | Wandering zero or plant-state-dependent spikes. | Follow the detector and receiving-system wiring diagrams; verify supply at load, polarity, segregation, earth and shield terminations. |
| Local-only test | Remote alarm or shutdown remains unavailable. | Head responds but panel event, beacon or interlock does not. | Run and record an end-to-end proof test, including restoration of bypasses. |
Maintenance handoff checklist
- Confirm the target gas list and sensing technology.
- Confirm the detector’s approval and environmental limits.
- Map credible release points and ventilation states.
- Inspect orientation, access, guards and inlet condition.
- Record contaminant and over-range exposure.
- Verify calibration gas, expiry, flow and adapter.
- Record as-found response before adjustment.
- Compare response time and value with acceptance limits.
- Witness local and remote alarms.
- Witness required interlocks and final actions.
- Record all inhited outputs and temporary safeguards.
- Confirm every bypass is removed after testing.
- Trend slow response and growing span correction.
- Approve replacement or coverage changes through management of change.
Related BuildMEP guidance
- Hydrocarbon leak sensors: selection and application guide
- NO2 vs CO detection for parking-garage ventilation control
- Tank-farm leak detection: lessons from Buncefield and ITC Deer Park
Evidence trail
- IEC 60079-29-2:2015, second edition—selection, installation, safe use and maintenance guidance for flammable-gas and oxygen detection equipment.
- IEC 60079-29-0:2025, first edition—current general requirements, test methods and acceptance criteria for gas-detection equipment.
- UK HSE: The selection and use of flammable gas detectors—maintenance, inspection, calibration and availability guidance.
- UK HSE safety alert: failure to detect gas due to an unsuitable sample tube—why the sampling path and target substance must be included in the response check.
- Honeywell Sensepoint XCD Technical Manual, Issue 9—product-specific bump-test, calibration-cap and test-gas application requirements.
- MSA Gas Detection Handbook—hazard analysis, leak-source mapping, airflow and accumulation considerations for detector placement.
Evidence boundary: this guide provides a maintenance and diagnostic framework, not a detector-coverage study, hazardous-area certification, alarm-setpoint design or substitute for the exact detector manual and adopted project requirements.
Frequently asked questions
Does a successful calibration prove a fixed detector is reliable?
No. It can verify or adjust zero and span under the prescribed test conditions. It does not by itself prove release coverage, unobstructed plume travel, remote alarm delivery, shutdown action or correct restoration of bypasses.
Should a methane detector always be installed at ceiling level?
No universal height rule is sufficient. Methane buoyancy matters, but release pressure and temperature, ventilation, roof geometry, obstacles and the monitoring objective also control placement. Follow a hazard-based placement study and the product instructions.
Can a hydrocarbon infrared detector detect hydrogen?
Conventional hydrocarbon IR sensors do not detect hydrogen. If hydrogen is credible, select a technology explicitly approved for hydrogen and verify its performance and environmental limits for the application.
What should be done after a detector fails a bump test?
Follow the exact manufacturer procedure. Keep the point out of safety service, provide temporary risk controls, verify the test gas and delivery path, perform the prescribed calibration or diagnostic checks, replace failed parts where required, and complete an end-to-end test before restoration.